If you’re building today’s electronics, chances are high you’ve used SMT. Since parts keep shrinking while assembly speeds up, older through-hole designs are slowly being replaced by surface-mounted versions. That change even covers simple bits like pin headers.
A small surface-mounted connector might speed up production – though it brings its own quirks. Meant for folks who build circuits and tweak layouts. Let’s dig into when they help, ways to dodge typical snags, plus solid tips that make designs work better.
What is an SMD Pin Header? The Shift to Surface Mount

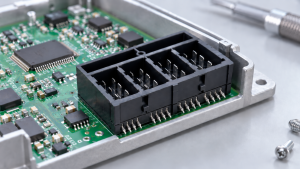
A small SMD pin header – also called an SMT type – is built to attach right onto flat spots on a circuit board’s top layer. Instead of poking holes through like old-school THT pins, these stay fully up front. Picture them resting gently atop the surface rather than running straight through.
This shift fits into a much bigger pattern across the sector. Moving toward Surface Mount Tech – handling everything from small resistors to advanced chips – happens because companies want devices that are tinier, smarter, built quicker, without spending too much. Though older through-hole parts stick around when a solid physical hold matters most, their role fades in mass manufacturing setups.
The Advantages of Using SMD Pin Headers
Switching from through-hole to a surface mount pin header isn’t just about following a trend. It offers real, measurable benefits in production and design.
Designed for Automated Assembly
The biggest plus of SMT parts? They work smoothly with auto assembly lines. SMD pin headers get grabbed and set by machines that place them exactly where needed. Because of this, things move super quickly and accurately – way faster than putting in THT bits by hand. That speed slashes both build time and worker expenses. In mass-produced gadgets, running on automation makes or breaks profit.
Enabling High-Density Designs
Since an SMD connector skips the need for holes in the PCB, space gets freed up. One big plus? More room means better layout options – also, it lets circuits pack tighter without losing function
- You’ve got extra room – fit parts on either side, facing one another.
- Routing gets simpler when there are no holes in the way – open paths let signals move freely across internal layers.
Smaller size comes from these elements, yet they still work just fine.
Improved Electrical Performance
Even though folks don’t always focus on this, surface-mount parts might handle electric signals more smoothly. Their leads are smaller, so electrons move across tighter routes. That cuts down side issues like hidden resistance or stored charge – stuff that messes with clean transmission when frequencies run high.
Key Challenges and How to Overcome Them
Even though they work well, SMD pin headers sometimes bring certain problems. No need to stress – knowing what’s going wrong helps fix it fast.
Challenge 1: Mechanical Strength
This is the biggest concern for most engineers. An SMD pin header is only held on by the solder on its surface pads. It lacks the anchoring strength of a THT pin that goes through the board. As a result, it can be ripped off the PCB if a connected cable is pulled too hard.
Solution: The Connector Selector’s Matrix—Balancing Strength, Cost, and Density
Choosing the right anchoring feature is not about always picking the strongest option; it’s about making the right trade-off for your product. We use a decision framework called the Selector’s Matrix to help guide this choice. Evaluate your design against these key criteria:
| Feature | Mechanical Stress | PCB Density | Assembly Cost/Complexity | Best For |
|---|---|---|---|---|
| Standard SMT | Low: Suitable for internal, non-handled connections. | Highest: No extra footprint space required. | Lowest: Standard SMT process. | Internal board-to-board links, like those often served by our standard 1.27mm & 2.54mm Pitch Headers |
| With Mounting Tabs | Medium: Greatly improves peel & shear strength. | High: Requires larger pads, but no through-holes. | Low: Still a single SMT process. | User-accessible ports in stable environments, a standard feature available in our Wire-to-Board Connector series |
| With TH Anchor Posts | Highest: Transfers stress to the PCB itself. Superb durability. | Lowest: Requires keep-out areas on both sides of the board. | Highest: Adds a through-hole soldering step (pin-in-paste or wave). | Industrial, automotive, or any product where the connector will face rough handling or high mating cycles. |
How to Use This Matrix:
Start by identifying your primary design driver. Is it cost? density? durability? Your primary driver will point you to the best starting option. For example, a ruggedized handheld scanner must prioritize durability, making TH Anchor Posts the clear choice, even at a higher cost.
Challenge 2: Reflow Soldering Compatibility
An SMD pin header must survive a trip through a reflow oven. This process, governed by the industry standard J-STD-020, defines specific temperature profiles that components must withstand. For lead-free soldering, peak temperatures can reach up to 265°C. A connector made from a standard plastic (like commodity PA66) with a low Heat Deflection Temperature (HDT) will melt, deform, or warp under these conditions, ruining your entire board.
Solution: Verify Material and Profile in the Datasheet
This is not a place to cut corners. You must select a header made from a high-performance thermoplastic specifically engineered for SMT processes. The critical property to verify in the datasheet is not just the material name, but its ability to meet a specific classification from the J-STD-020 standard.
Look for these materials, which are chosen for their high HDT:
- LCP (Liquid Crystal Polymer): The “gold standard” due to its exceptional dimensional stability and very high HDT, often exceeding 280°C.
- PA9T, PA6T, or HTN (High-Temperature Nylon): Excellent, often more cost-effective alternatives that also offer the necessary thermal stability to withstand lead-free reflow profiles.
Always cross-reference the component’s datasheet with your assembly partner’s capabilities. Look for the “Recommended Reflow Profile” graph in the datasheet. This graph is your assurance that the part is designed to survive a specific time-temperature curve without damage.
Expert Insight: Don’t Always Default to LCP
While datasheets rightly praise LCP (Liquid Crystal Polymer) as the “gold standard” for high-temperature performance, defaulting to it can be an expensive mistake.
The Conventional Wisdom: Choose LCP for maximum thermal safety margin.
The Original Method: A more cost-effective approach is to “design for your process.” If your assembly partner has modern ovens with precise thermal profiling and your PCB design doesn’t have large thermal masses near the connector, a high-temperature Nylon like PA9T can often provide sufficient performance at a 15-30% component cost reduction. The key is to analyze the actual thermal load the component will see on your board, not just the theoretical maximum of the reflow oven. Discussing this trade-off with your connector supplier and CM can yield significant savings without compromising reliability.
SMD Pin Header Design & Layout Best Practices
A successful design goes beyond just picking the right part. How you design your PCB footprint is just as important.
Follow Datasheet Footprint Recommendations
The single most important rule is to strictly adhere to the manufacturer’s recommended PCB footprint. This is not just a suggestion; it’s a critical design requirement. Manufacturers invest significant R&D to define these layouts based on the principles of IPC-7351 (Generic Requirements for Surface Mount Design and Land Pattern Standard).
The goal is to create a land pattern that ensures the ideal solder fillet formation (the shape of the solder connecting the pin to the pad) for three key areas: the toe, the heel, and the sides of the pin. A correct fillet is the basis for both mechanical strength and a low-resistance electrical connection. Don’t try to guess or create your own; use your CAD software to precisely replicate the dimensioned drawing found in the component datasheet. Deviating from this can directly lead to assembly defects like opens, shorts, or mechanically weak joints that fail under stress.
Packaging for Automation
How the parts arrive at your factory matters. SMD pin headers are typically supplied in a few ways for automated machines:
- Tape & Reel: The most common format. Parts are placed in pockets of a plastic tape wound onto a reel. Some headers may require a small plastic pick-and-place
capor film on top so the machine’s vacuum nozzle has a flat surface to grab. - Tube (or Stick): Parts are stacked in a rigid plastic tube.
Your assembly partner will tell you what format their machines prefer, but Tape & Reel is the industry standard.
Common SMD Header Configurations
Like their THT cousins, smd pin headers come in many shapes and sizes to fit different layouts. The most common are:
- Vertical: The pins point straight up, perpendicular to the board surface.
- Right-Angle: The pins are bent and lie parallel to the board surface, used for edge connections.
- Dual-Row: Two rows of pins for higher-density connections.
Partner with a Manufacturing Expert
Selecting the right SMD pin header is more than just matching a pitch and pin count; it’s about ensuring long-term reliability and manufacturing efficiency.
At SOULIN, we don’t just sell connectors—we provide engineering solutions. Our team is ready to help you:
- Review your design for optimal connector selection.
- Provide detailed datasheets, 3D models, and footprint files for our parts.
- Discuss customization options for unique application requirements.
Don’t leave your product’s reliability to chance. Contact the SOULIN engineering team today to discuss your next project.